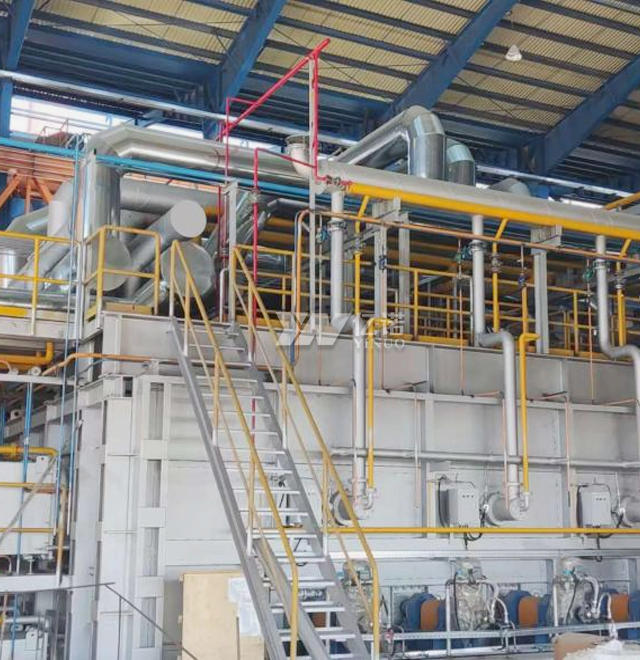
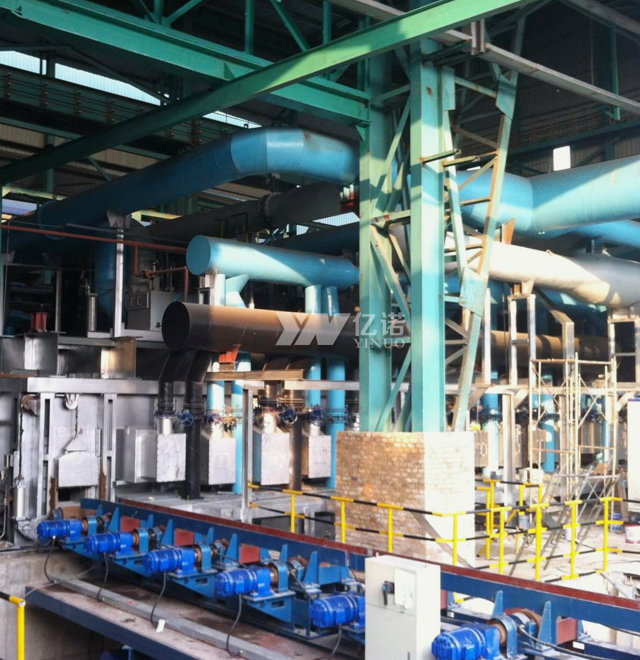
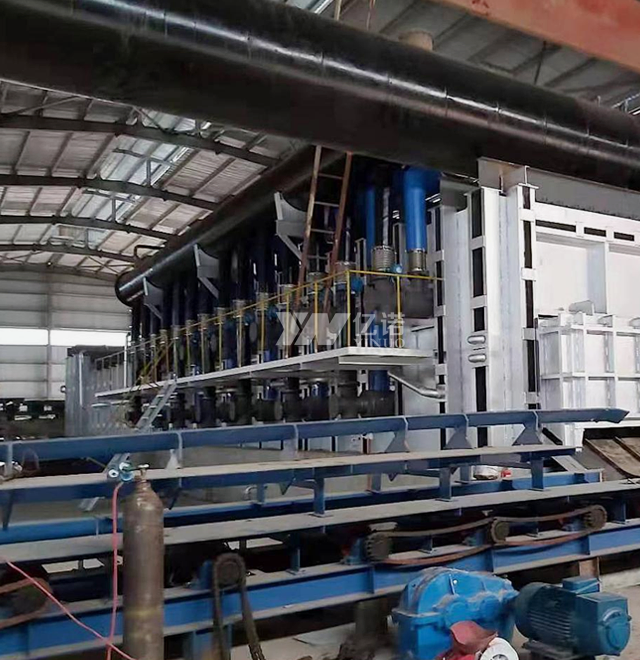
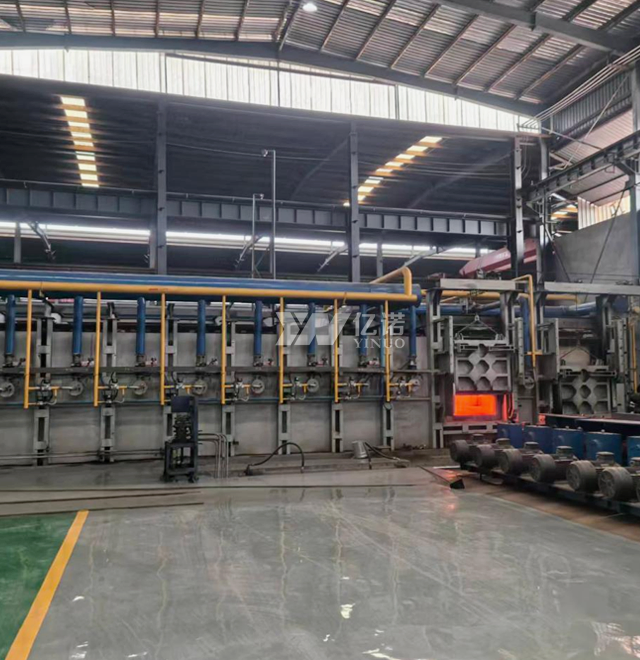
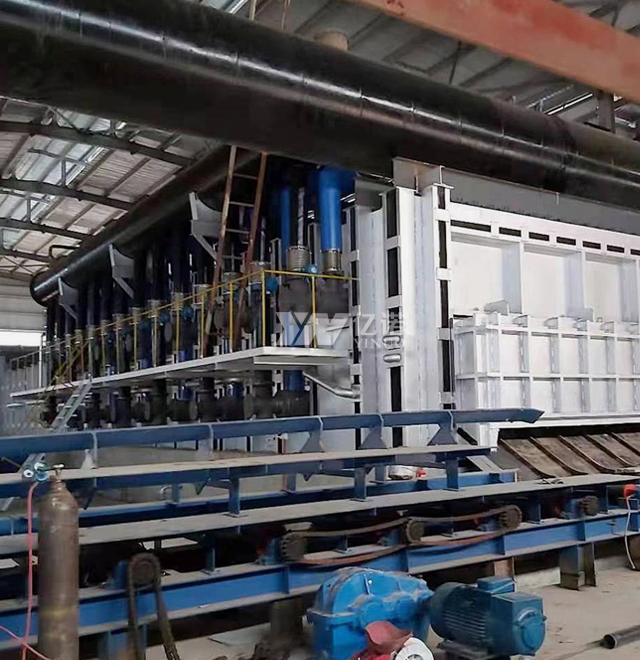
Walking Beam Furnace Burner Management System – Advanced Safety & Automation Solution for Steel Reheating
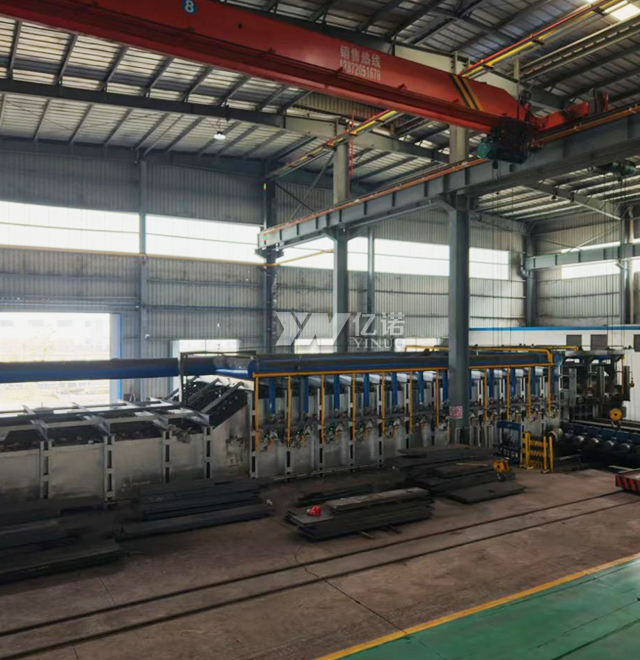
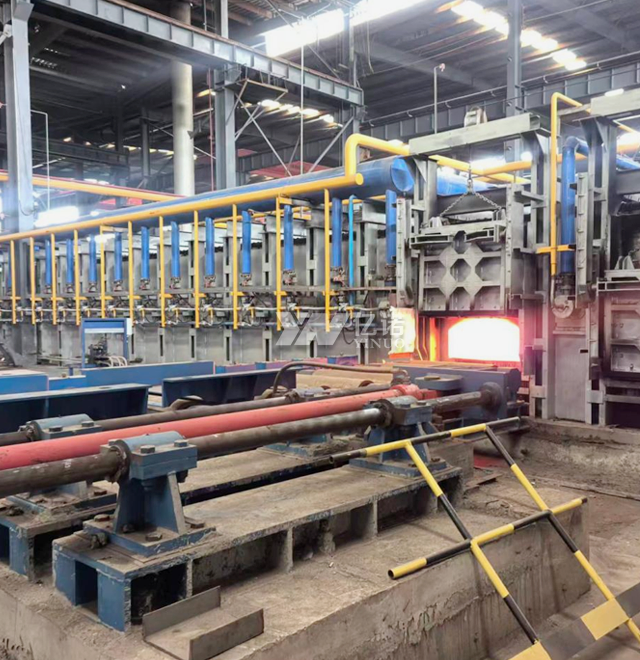
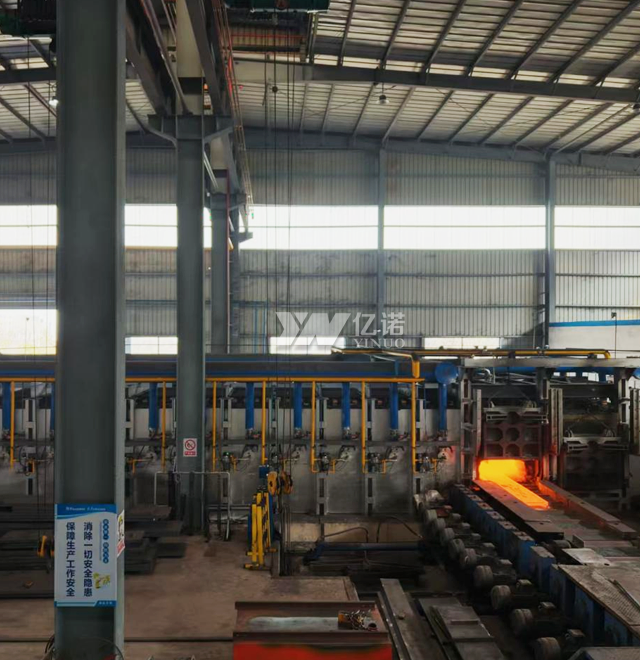
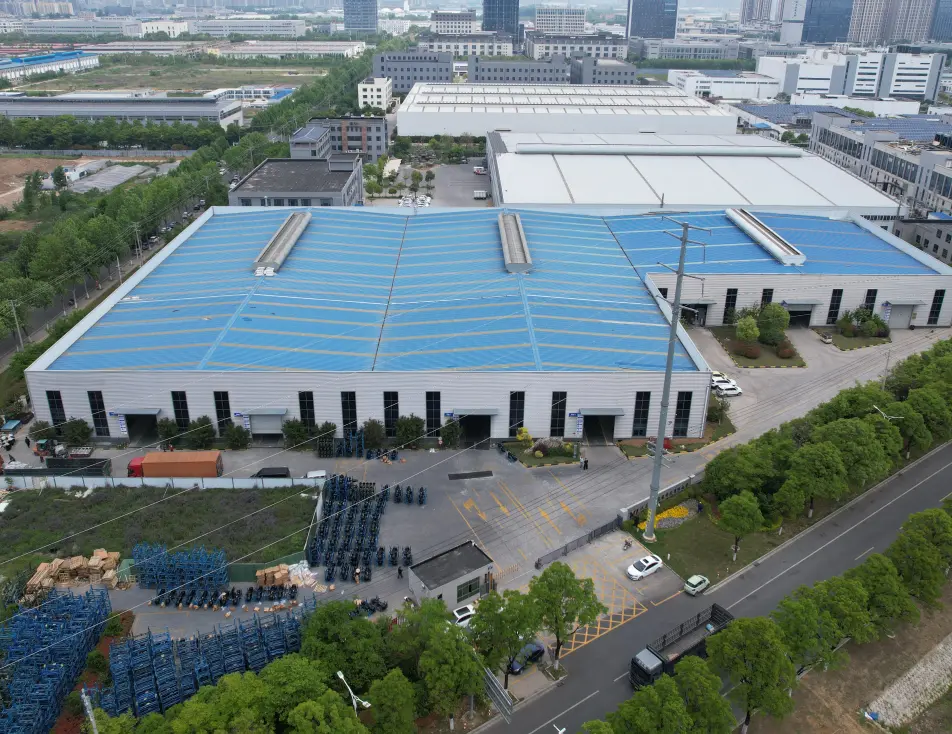
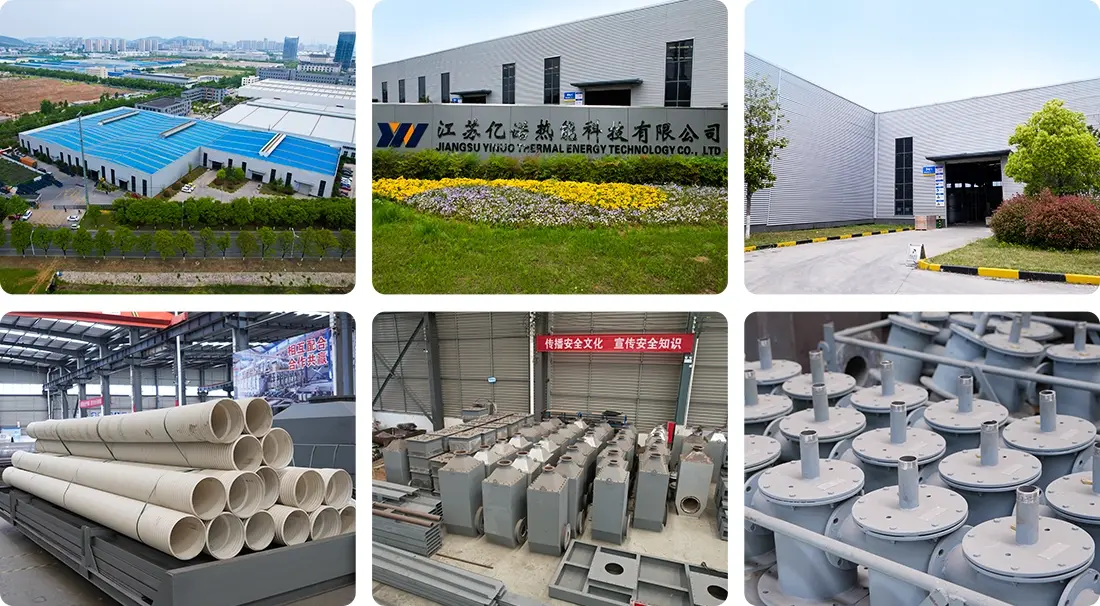
The Walking Beam Furnace Burner Management System comes from JIANGSU YINUO THERMAL ENERGY TECHNOLOGY. Steel mills that run at high capacity use it. Over 100 specialists work at the company. Its plant covers 20,000㎡. Fixed assets reach 80 million yuan. One package holds the safety interlock logic, the multi-zone combustion control and the real-time flame monitoring. Slabs heat at up to 350 t/h. Billets reach 200 t/h. Heat stays between 1150–1250°C. Oxidation loss comes in below 0.9%. Energy use is ≤1.05 GJ per ton of steel.
What Makes Our Burner Management System Different?
Several heating zones fall under its watch. The full burner lifecycle gets covered too, from ignition sequences through to emergency shutdowns. A catastrophic explosion can start with fuel buildup. Stopping that is a constant pressure on you. Even temperature profiles across very large workpieces have to be held at the same time.
Those challenges get answered by a Safety Integrity Level (SIL) 2/3 compliant architecture. At the core sits a modular PLC design. Two redundant UV/IR flame scanners separate a real burner flame from background refractory glow, and extreme heat does not fool them. Automated purge cycles clear 4-10 furnace volumes before ignition. Leaks get spotted as they happen by Valve Proving Systems.
Profinet or Modbus TCP/IP ties this setup to the Combustion Control Systems. Air-fuel ratio tuning then becomes precise. Thermal efficiency stays where it should be. Interlock conditions get watched by a separate safety layer that runs on its own. Fuel cuts off in under 4 seconds if anything goes wrong.
Technical Specifications
| Parameter |
Value |
| Applicable Fuels |
Blast Furnace Gas, Mixed Gas, Producer Gas, Natural Gas |
| Heating Capacity |
Max. 350 t/h (Slab); Max. 200 t/h (Billet) |
| Temperature Range |
1150–1250°C |
| Unit Heat Consumption |
≤1.05 GJ per ton of steel |
| Oxidation Loss Rate |
<0.9% |
| Flame Detection Response |
<2-4 seconds |
| Safety Compliance |
NFPA 86, EN 746-2, ISA 84 |
| Control Architecture |
Siemens S7-1500H / Allen-Bradley GuardLogix |
| Walking Beam Cooling |
Water cooling / Evaporative cooling |
| Customization |
Available per customer requirements |
Where You Can Apply This Technology
Hot Rolling Mill Reheating: On your high-tonnage lines, managed high-velocity burners keep reheating at exactly 1,250°C. Mechanical vibration comes along with beam movement. The Walking Beam Furnace Burner Management System compensates for it. Flame conditions then hold steady through the whole heating cycle.
Seamless Pipe Heat Treatment: Quenching and tempering need ±5°C uniformity. Multi-zone pulse-firing control keeps that spread steady over the full hearth. Metallurgical properties come out repeatable. That matters in critical applications.
Aluminum Slab Homogenizing: some sites run the process at lower temperatures. Air-recirculation volumes are high. That setup needs special low-NOx burner management. The system guards against one risk: localized overheating. It keeps the structure of aerospace-grade alloys intact.
Quality Assurance You Can Trust for Walking Beam Furnace Burner Management System
Harsh steel-mill conditions demand strict inspection. We build those protocols into every project:
Before shipment, Factory Acceptance Testing runs a digital twin simulation. Logic sequences get checked this way. So do emergency shutdown triggers. Flame Signal Intensity Verification makes sure your sensors tell a working flame apart from thermal background noise.
Valve Train Tightness Testing follows ISO 23550. It proves fuel shut-off valves do not leak. Electromagnetic Compatibility Testing keeps high-power walking beam drive motors from causing interference. Field-mounted control cabinets face ambient temperatures above 60°C. Environmental Stress Screening shows how they hold up.
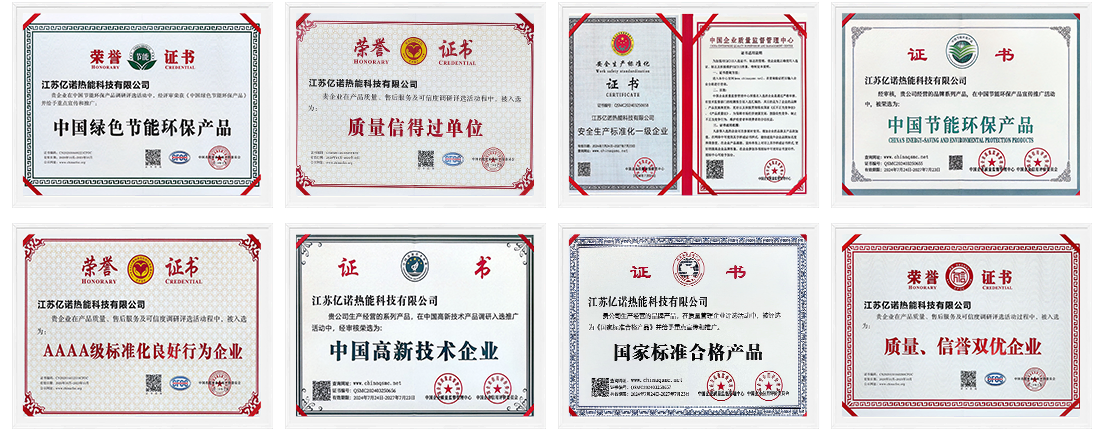
Every system component gets checked by our Walking Beam Furnace Burner Management System quality inspection department. The checks follow national and industrial standards. With each delivery you get test results and certification on paper.
FAQ
Q: How does the system handle nuisance trips during furnace startup?
A: Smart flame discrimination does the watching. Purge timing is tuned to match. Together they hold ignition steady, and the NFPA 86 safety interlocks stay wired in the whole time. Operators hear fewer false alarms. Safety does not drop.
Q: Will this setup retrofit onto older manual furnaces?
A: Yes. Brownfield upgrades are most of what we do. Out comes the old relay logic, in go SIL-rated PLCs and flame scanners that read fast. Existing assets get brought up to date. No full replacement needed.
Q: In this setup, what makes the BMS different from the CCS?
A: The BMS is the safety layer. It handles interlocks and fuel shut-off. The CCS takes care of process variables such as temperature and air-fuel ratio. The two systems talk to each other, yet their safety functions stay separate.
Q: What happens when atomizing air or fuel pressure is lost?
A: Affected burners shut down right away, and a supervisor oversees every step. That takes milliseconds. Hazardous gas never gets a chance to build up. Even when the utility supply fails, your facility stays protected.
Q: Is remote monitoring supported?
A: Yes, the system includes secure gateway protocols for IIoT integration, allowing remote diagnostics and predictive maintenance of valve actuators and flame sensors. You reduce downtime through early anomaly detection.
Partner With Thermal Energy Experts
Ready to enhance your furnace safety and efficiency with Walking Beam Furnace Burner Management System? Contact our specialists at info@yinuofurnaces.com to discuss your specific requirements.